Custom Screen Printing
Bold color, crisp detail, and ink that stays put wash after wash. Printed in house in Urbana, Ohio.
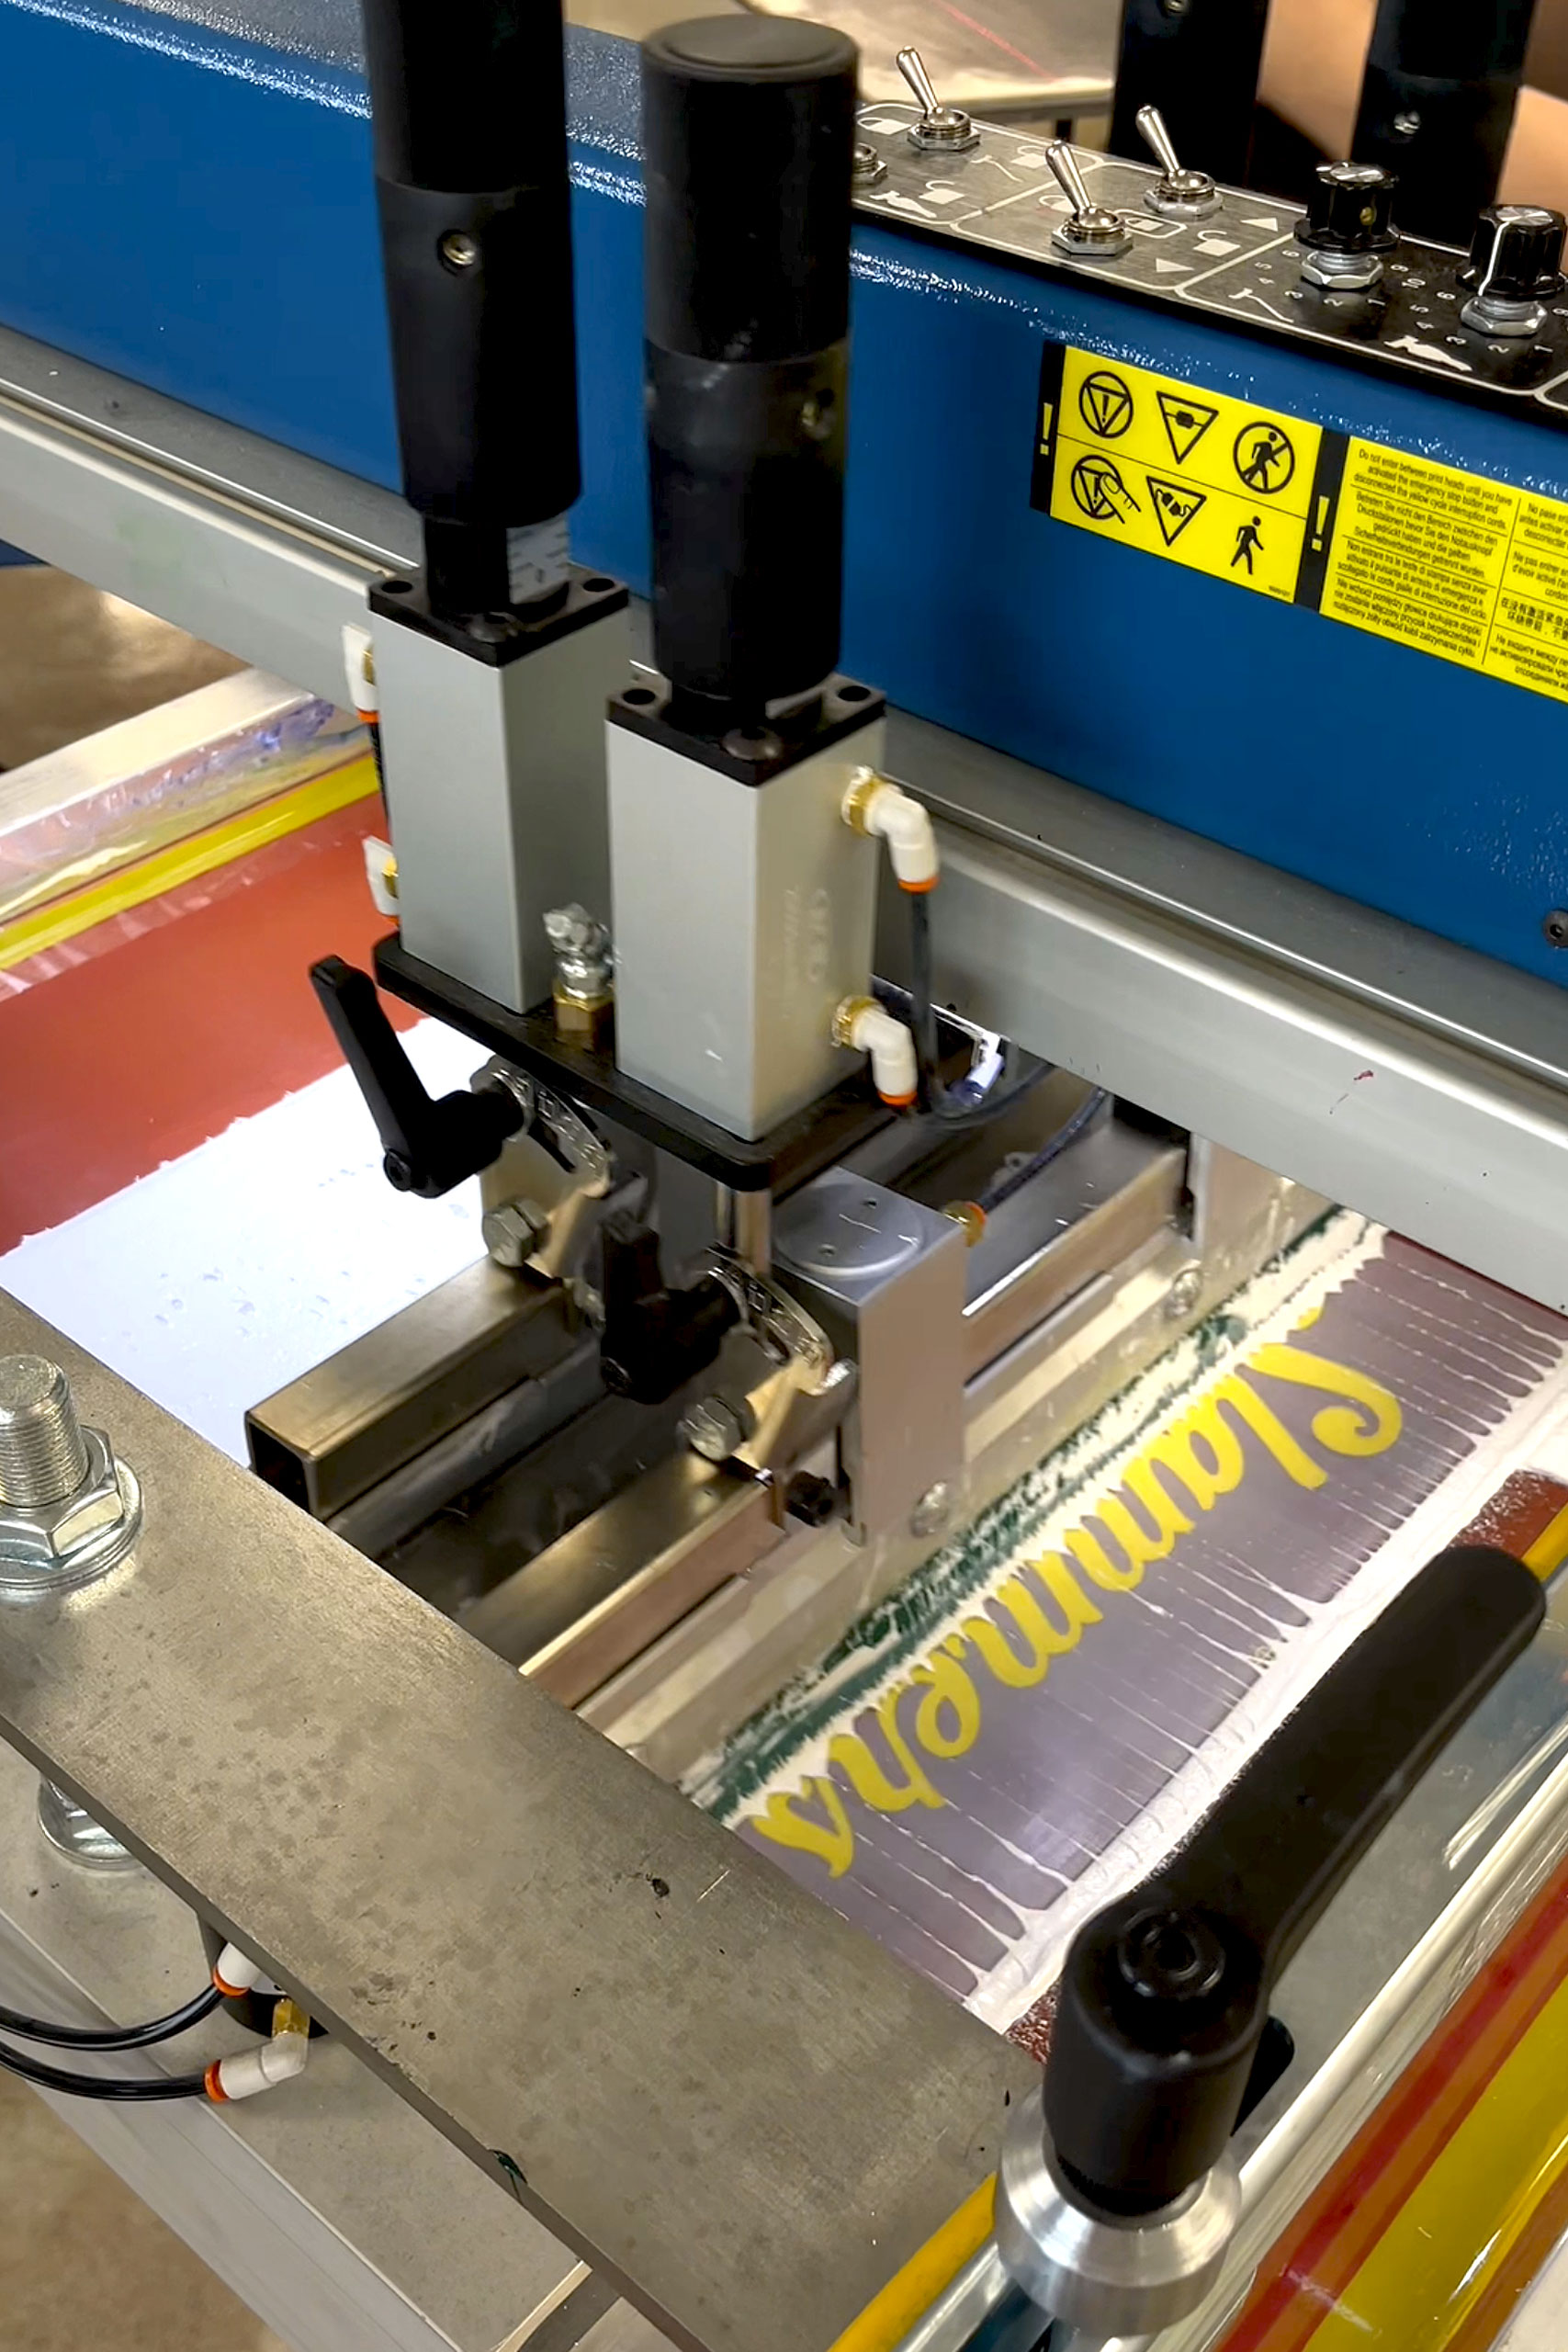
Screen printing is the workhorse of custom apparel, and we treat it like a craft. Every job runs on our own presses, gets cured to spec, and gets checked before it ships. Team tees, event shirts, crew hoodies, workwear:
if it needs bold color that lasts, this is the method.
Custom T-shirt printing that holds up
A screen print lasts as long as it was cured correctly. Plastisol ink has to reach roughly 320°F through the entire ink layer to bond with the fabric. Cut that short and the print cracks after a few washes. We run an adhesion test on every job before full production, so the ink on shirt 1 matches the ink on shirt 300.
Properly cured screen prints hold up through well over 100 washes. That durability is why screen printing remains the go to for team apparel, uniforms, and anything printed at volume.
320°F
Cure temp through the ink layer
100+
Washes when cured right
What can we screenprint?
T-shirts and Tanks
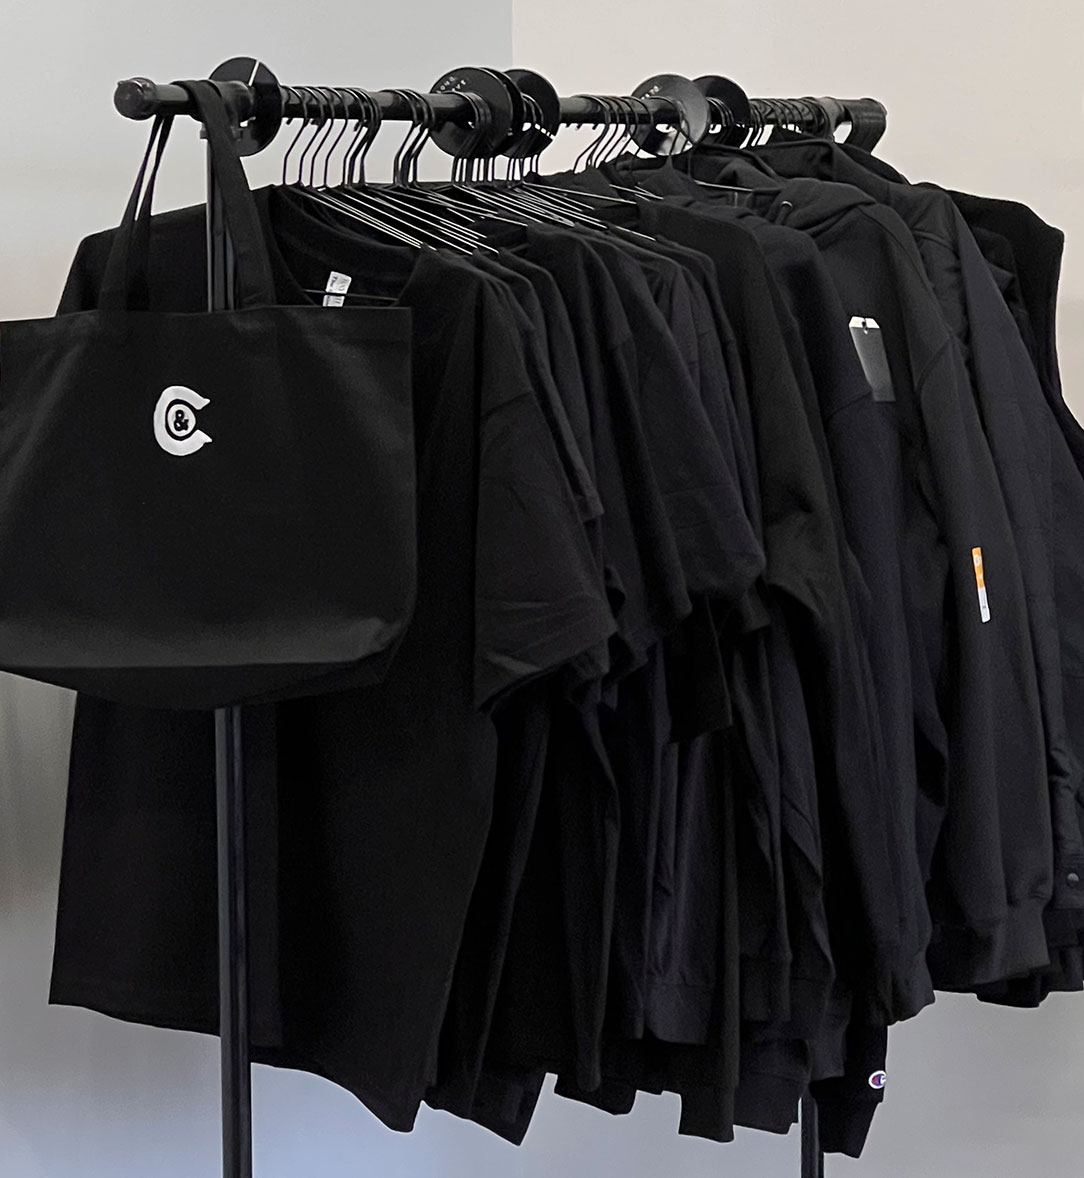
The core of most orders. We print on everything from budget friendly blanks to soft, side seamed ring spun tees from Bella+Canvas, Next Level, and Comfort Colors.
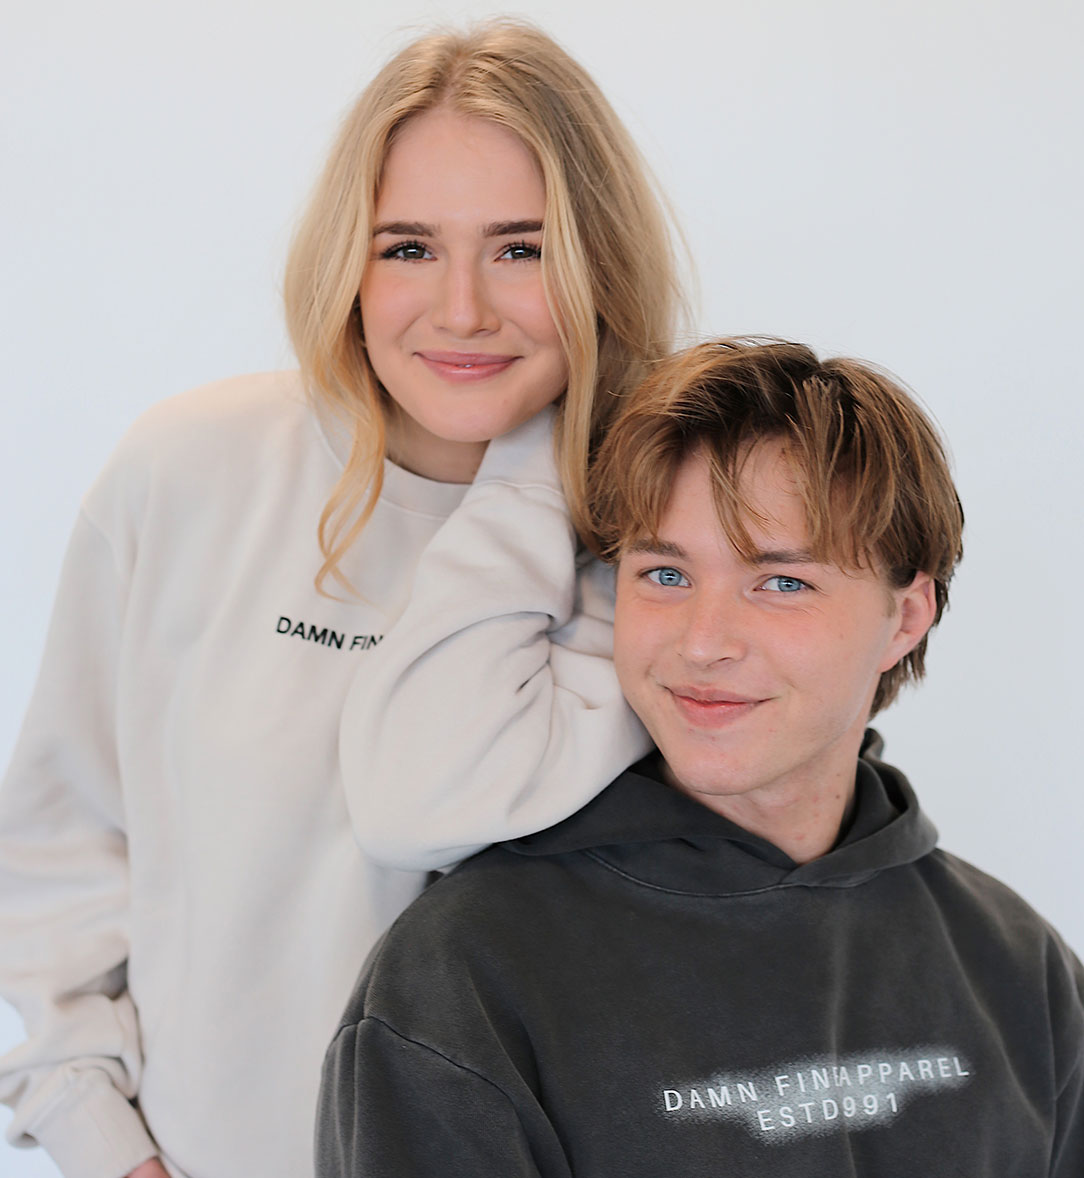
Hoodies and Sweatshirts
Front, back, and sleeve prints on heavyweight fleece. Ideal for crews, schools, and company apparel that gets worn all winter.
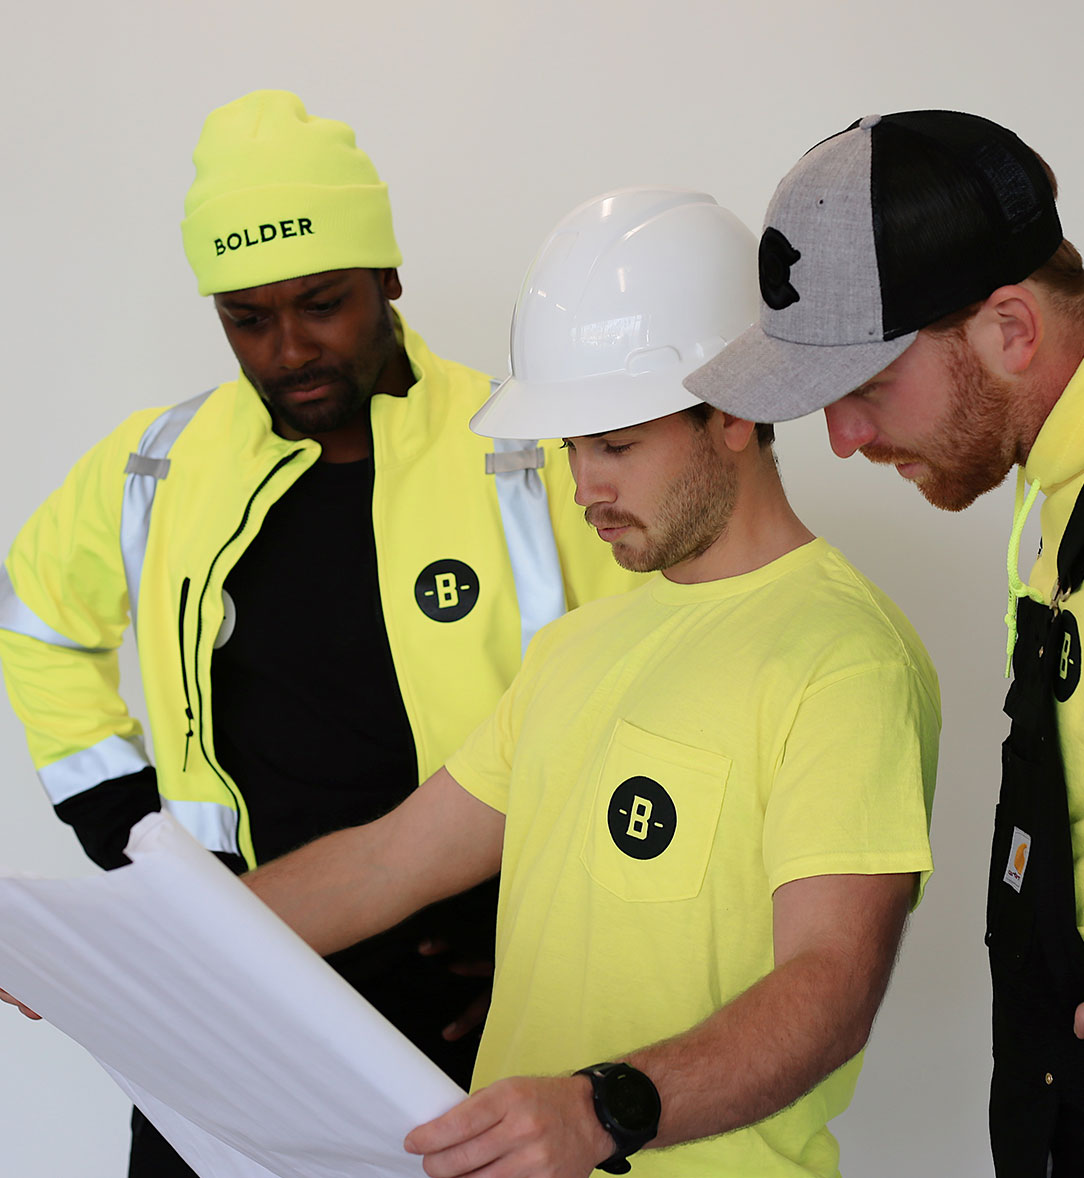
Workwear
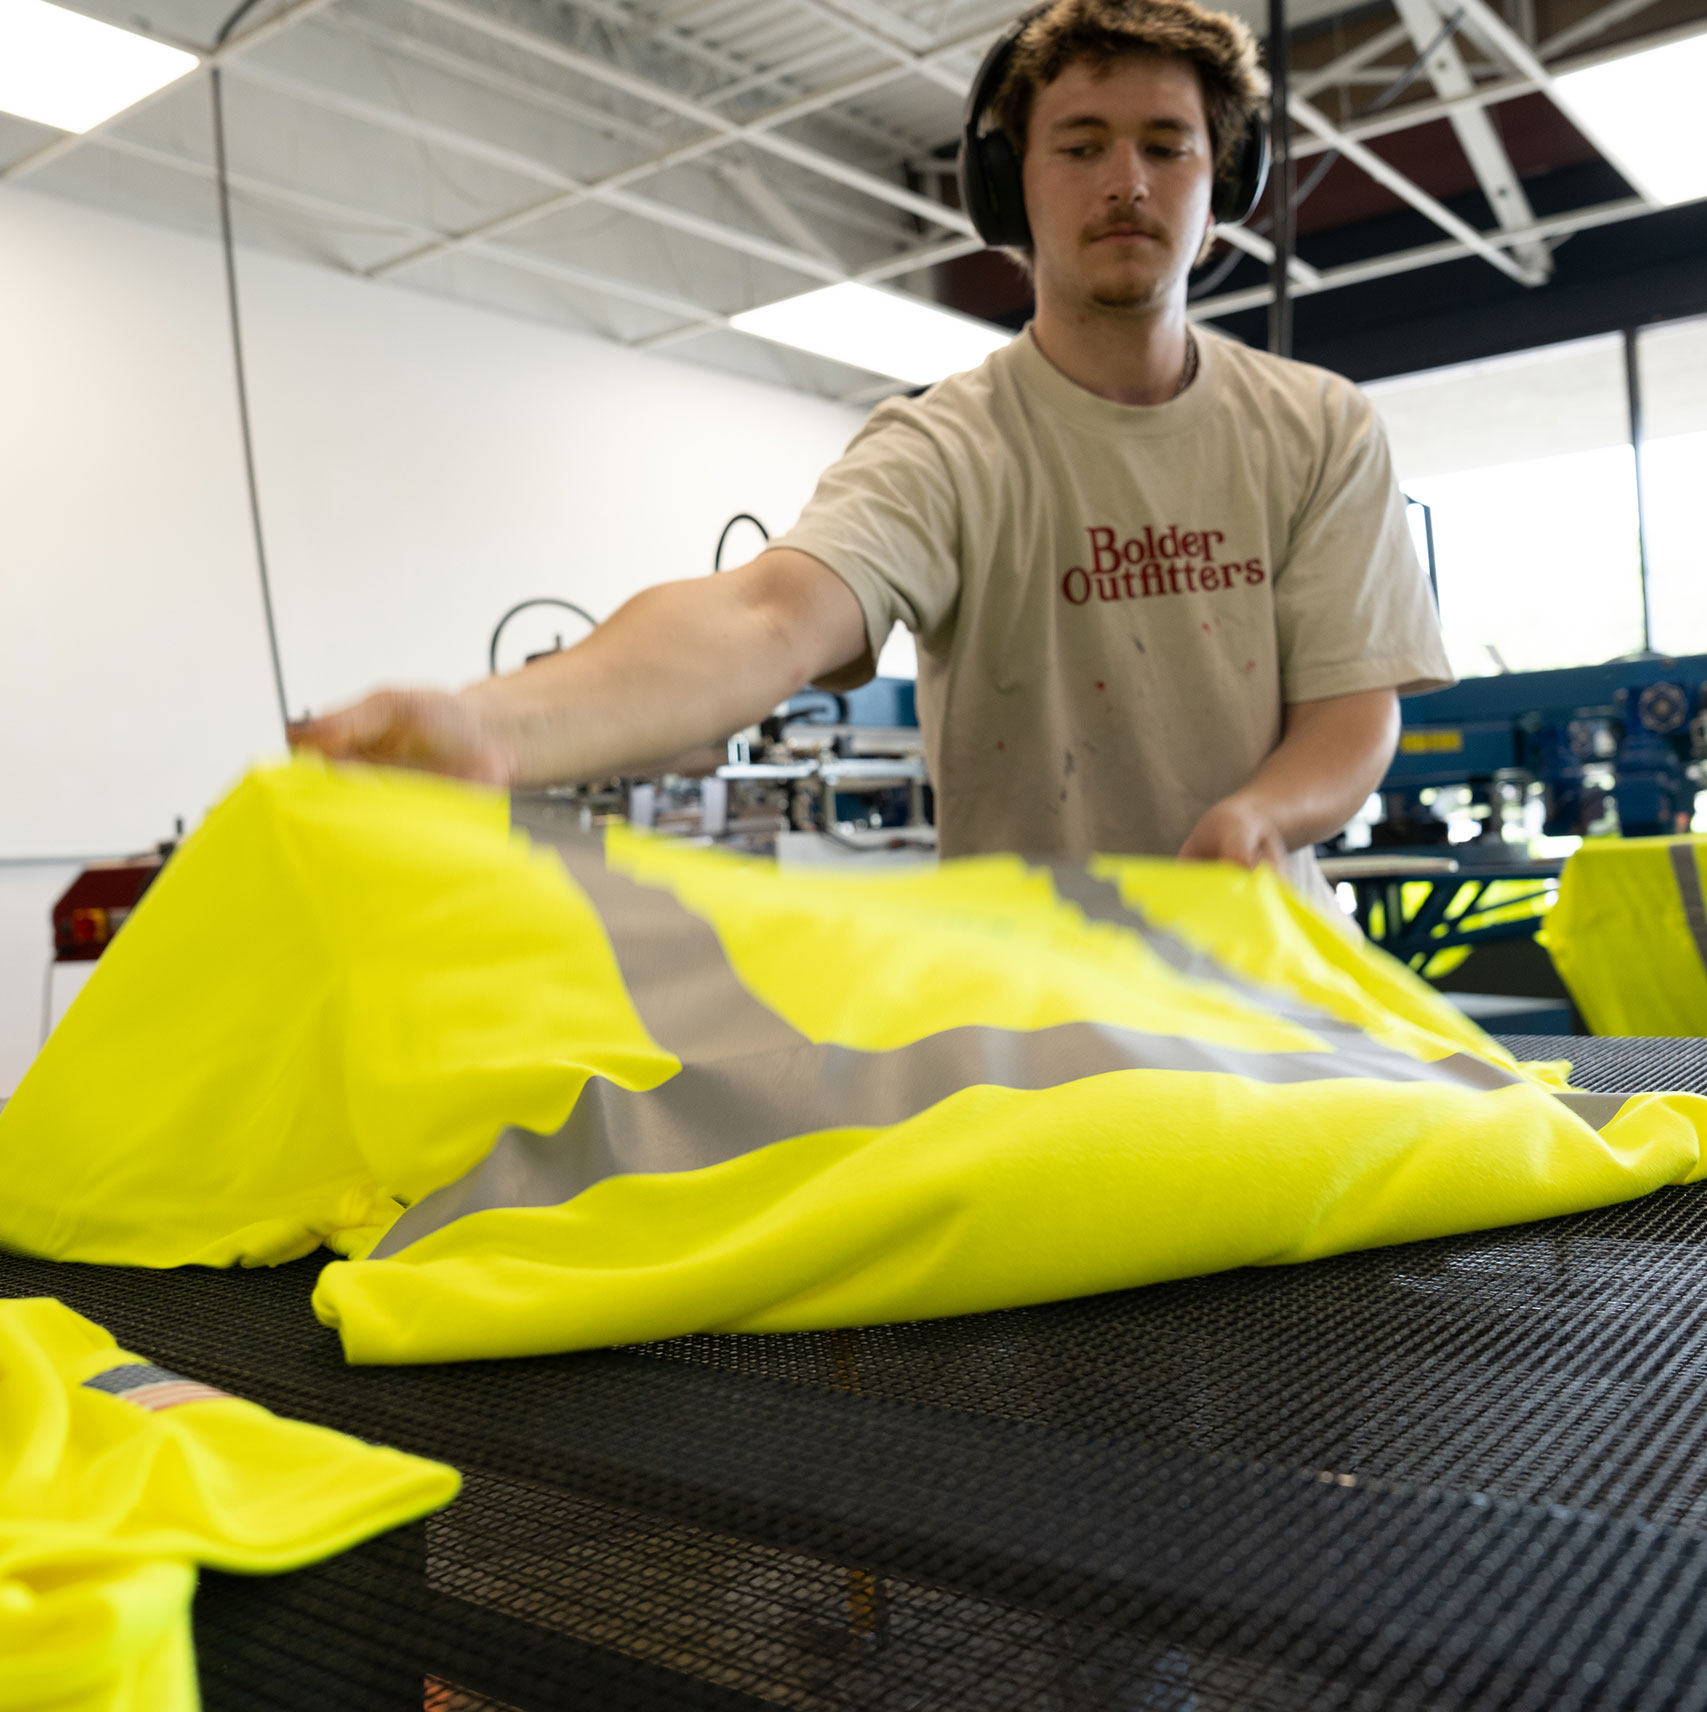
Durable prints on Carhartt, Dickies, and hi vis garments, placed to preserve safety striping and compliance areas.

Totes and Accessories
Canvas totes, aprons, and other flat goods that take ink cleanly.
When is screen printing the right choice?
Screen printing wins on larger orders with bold, limited color designs. Setup happens once per color, so the cost per piece drops as quantity climbs. For a 2 color logo on 200 tees, nothing beats it on price.
For highly detailed or photographic artwork, heat transfer can be the better fit. For polos, hats, and outerwear where a premium finish matters, embroidery usually leads. Our guide to embroidery, heat transfer, and screen printing compares all three, and our embroidery services cover the stitched side.
How does our screen printing process work?
01.
Art and color seperation
We review your file for resolution and print size, then separate the design into individual colors. Each color gets its own film.
02.
Burning the screens
Each film gets exposed onto an emulsion coated mesh screen. Mesh count is matched to your design, lower for bold coverage and higher for fine detail.
03.
Printing
Screens are registered so every color lines up, then ink is pulled through the mesh onto each garment. Multi color jobs get a flash cure between colors to keep layers clean.
04.
Curing and Quality check
Every garment runs through our conveyor dryer, then gets inspected before packing. For the full walkthrough, see what happens when we screen print your order.
How do you pick the right blank?
The garment shapes how the print looks and how long people wear it. Ring spun cotton prints cleaner and softens with wear, while budget blanks make sense for single use event shirts. We’ll recommend a blank with your quote, and our guide to the best blank tees for custom printing breaks down the options.




Screen Printing FAQ
What is the minimum for screen printing?
48 pieces for new customers.
How many colors can you print?
Each color in a design gets its own screen, so more colors mean more setup and a higher per piece cost. For full color or photographic artwork, we'll recommend a decoration method that reproduces it cleanly.
What file should I send?
Vector files work best: .AI, .EPS, .SVG, or a high resolution .PDF. If you only have a .PNG or .JPG, it should be at least 300 DPI at print size. If your file isn't ready, Bolder Creative can prep it.
How long does a screen printing order take?
About 2 weeks from proof approval for standard orders. Faster proof approval means faster delivery.
Ready to Print?
Send your logo, garment, quantity, and deadline. We’ll get you a quote the same day.
